A high-quality amine cooler is important in refinery service because it directly affects the performance, reliability, and safety of the whole amine treating unit. In an oil refinery, the amine system is used to remove acid gases such as H₂S and CO₂ from fuel gas, LPG, natural gas, or process gas. If the amine cooler does not work properly, the absorber may not remove acid gas effectively, and this can lead to off-spec gas, corrosion risk, and unstable plant operation.
The main job of the amine cooler is to reduce the temperature of lean amine before it returns to the absorber. Cooler lean amine usually has better acid gas absorption performance. If the lean amine enters the absorber at too high a temperature, the system may need a higher circulation rate, the treated gas quality may become unstable, and the regenerator load may increase.
In refinery operation, an amine cooler also faces difficult working conditions. The amine side may contain degradation products, heat-stable salts, hydrocarbons, iron sulfide, and suspended solids. The cooling water side may suffer from scaling, fouling, biological growth, or corrosion. A low-quality exchanger can lose heat transfer capacity quickly, causing higher outlet amine temperature and frequent maintenance.
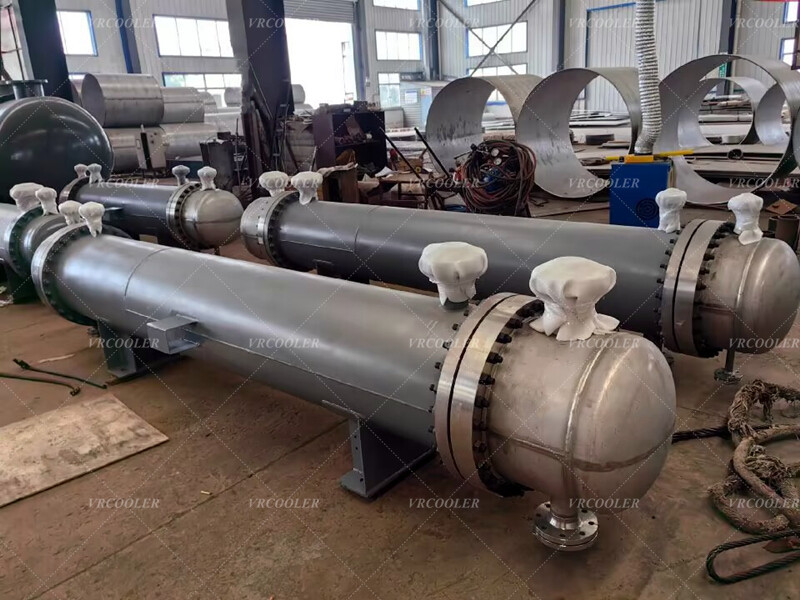
A well-designed shell and tube amine cooler offers several long-term advantages:
- Stable lean amine outlet temperature
- Better H₂S and CO₂ removal efficiency
- Lower risk of off-spec treated gas
- Better resistance to corrosion and fouling
- Easier cleaning, inspection, and tube replacement
- Longer service life in continuous refinery operation
- Reduced unplanned shutdown risk
- Lower long-term operating and maintenance cost
Material selection is especially important. Depending on the amine type, acid gas loading, chloride content, cooling water quality, and refinery standard, the exchanger may require carbon steel, stainless steel, duplex stainless steel, CuNi, titanium tubes, or special alloy materials. For seawater cooling or severe corrosion service, ordinary materials may fail too quickly.
For refinery users, the amine cooler should not be selected only by price. It should be selected according to process duty, amine concentration, operating pressure, inlet and outlet temperatures, fouling factor, corrosion allowance, pressure drop, cleaning method, and maintenance access.
In simple terms, a high-quality amine cooler helps the refinery keep the amine treating unit stable, efficient, and safe. It protects gas sweetening performance, reduces corrosion problems, saves operating cost, and supports long-term continuous production. For this reason, choosing a reliable customized shell and tube amine cooler is a practical investment for refinery service.